English
- English
- беларускі
- Hrvatski
- Тоҷикӣ
- O'zbek
- Español
- Português
- русский
- Français
- 日本語
- Deutsch
- tiếng Việt
- Italiano
- Nederlands
- ภาษาไทย
- Polski
- 한국어
- Svenska
- magyar
- Malay
- বাংলা ভাষার
- Dansk
- Suomi
- हिन्दी
- Pilipino
- Türkçe
- Gaeilge
- العربية
- Indonesia
- Norsk
- تمل
- český
- ελληνικά
- український
- Javanese
- فارسی
- தமிழ்
- नेपाली
- български
- ລາວ
- Latine
- Қазақша
- Euskal
- Azərbaycan
- Slovenský jazyk
- Lietuvos
- Eesti Keel
- Română
- Slovenski
- Srpski језик
Products
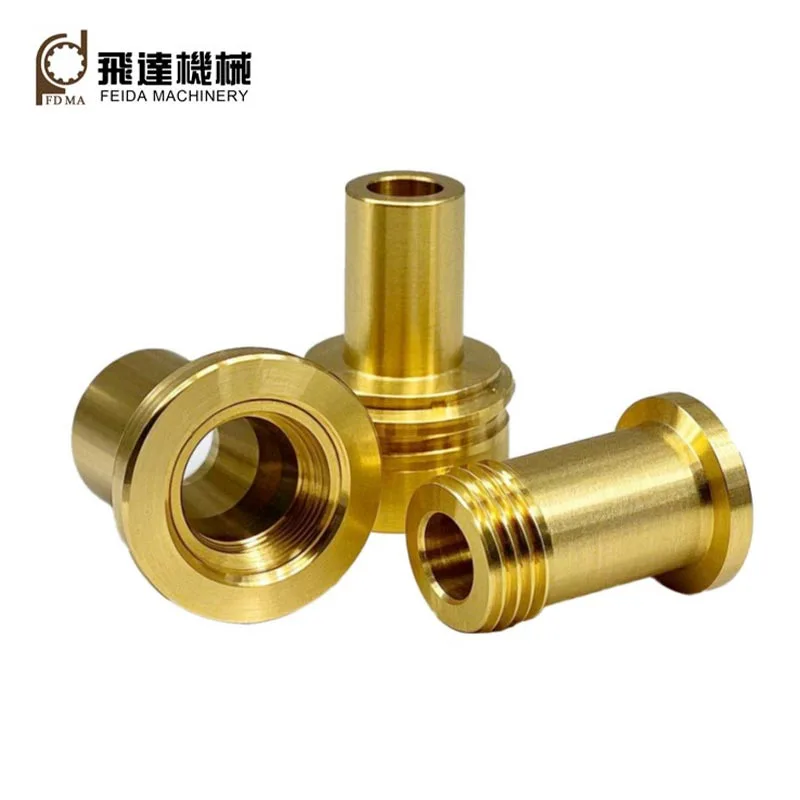
Brass Machining Hardware Fittings
For high-volume plumbing, pneumatic, and electrical assembly programs, sourcing dependable Brass CNC Turned Components and Copper Alloy Machined Fittings from a single precision machining partner reduces supply chain risk and improves part-to-part consistency. The catalog also includes Precision Brass Threaded Inserts for molded plastic bosses and Custom Copper CNC Turned Parts for thermal and electrical hardware. Every batch is machined on automated CNC lathes and machining centers, with in-process control of dimensional stability, thread fit, and surface quality.
The Brass Machining Hardware Fittings series is engineered for demanding fluid and electrical connection systems. Each component starts from solid bar stock or precision-cast blanks and is processed on multi-axis CNC lathes, Swiss-type lathes, and vertical machining centers. Programmed cutting speeds and feed rates are matched to brass and copper alloys to avoid built-up edge, maintain tight tolerances, and preserve clean thread profiles. Standard production covers male and female adapters, elbows, tees, unions, bushings, locknuts, hose barbs, compression sleeves, flared fittings, and custom manifold bodies. Threads are cut, milled, or rolled to ISO 965 and ASME B1.1 class 2A/2B as standard, with class 3A/3B available for precision assemblies. Internal bores are reamed and deburred to remove sharp edges, and sealing faces are turned flat or angle-controlled for reliable metal-to-metal or O-ring contact. Typical applications include water distribution, compressed air, fuel systems, hydraulic test stands, medical gas terminals, automotive brake fittings, marine hardware, and HVAC control valves. For low-lead drinking water compliance, C69300 lead-free brass and C87850 Eco Brass are available. Pressure ratings vary by geometry and thread size, with standard parts tested to 150 psi for NPT assemblies and 250 psi for BSPT assemblies. Dimensional inspection uses calibrated calipers, micrometers, optical comparators, and coordinate measuring machines. Tool life is monitored with automatic wear offsets, and periodic sampling confirms that root and crest radii remain within drawing limits. For sealing surfaces, circularity is held within 0.01 mm to prevent leakage at assembled joints. Light chamfers are applied at all thread entry points to protect mating components during installation. When secondary operations such as grooving for O-rings or drilling for safety wire holes are required, they are completed in the same setup to reduce handling variation. Parts are individually inspected for thread go/no-go acceptance and visual surface defects. Packaging options include bulk polybags, compartmented trays, and custom foam inserts for high-value assemblies. Small-batch prototype orders are typically completed within 7–10 working days, while production runs above 5,000 pieces are scheduled through dedicated cells to hold unit cost stable. Custom laser marking, part numbering, and barcode labeling are available for traceability. Electroless nickel and bright tin plating are performed in-house, while silver, gold, and zinc-nickel finishes are sourced from certified partner lines. Plating thickness is verified by X-ray fluorescence on each lot, and adhesion is checked by thermal shock testing on sample parts.
- Material Grades: C36000 free-cutting brass, C37700 forging brass, C38500 architectural brass, C11000 ETP copper, C14500 tellurium copper.
- Machining Capability: Multi-axis CNC turning, milling, drilling, tapping, knurling, grooving, thread whirling, and cross-drilling.
- Diameter Range: From 3 mm to 120 mm (0.118" to 4.724"); lengths from 5 mm to 300 mm (0.197" to 11.811").
- Thread Standards: ISO metric M2–M42, UNF/UNC #0–1-1/2", BSPP/BSPT 1/8"–2", NPT 1/8"–2".
- Tolerance Control: ±0.005 mm on turned diameters, ±0.01 mm on lengths, angular tolerance ±0.1°.
- Surface Finish: Ra 0.4–1.6 µm as standard; deburred, passivated, and oil-free parts available.
- Plating and Coating: Electroless nickel, bright tin, silver, gold, zinc-nickel, and black oxide.
- Quality Assurance: ISO 9001:2015 certified inspection, CMM reports, material certificates, PPAP level 3 on request.
| Parameter | Standard Specification | Optional / Custom Range |
|---|---|---|
| Material Grades | C36000 brass, C11000 copper | C37700, C38500, C14500, C69300 lead-free brass |
| Outer Diameter | 6 mm to 60 mm | 3 mm to 120 mm |
| Length | 10 mm to 150 mm | 5 mm to 300 mm |
| Thread Size | M3 to M24, 1/8" to 1" NPT/BSP | M2 to M42, up to 2" |
| Surface Roughness | Ra 1.6 µm | Ra 0.4 µm mirror finish |
| Plating Thickness | Nickel 3–5 µm | Silver 5–15 µm, gold 0.5–3 µm |
| Inspection Standard | ISO 2859-1 AQL 0.65 | 100% CMM inspection, PPAP |
Related Products
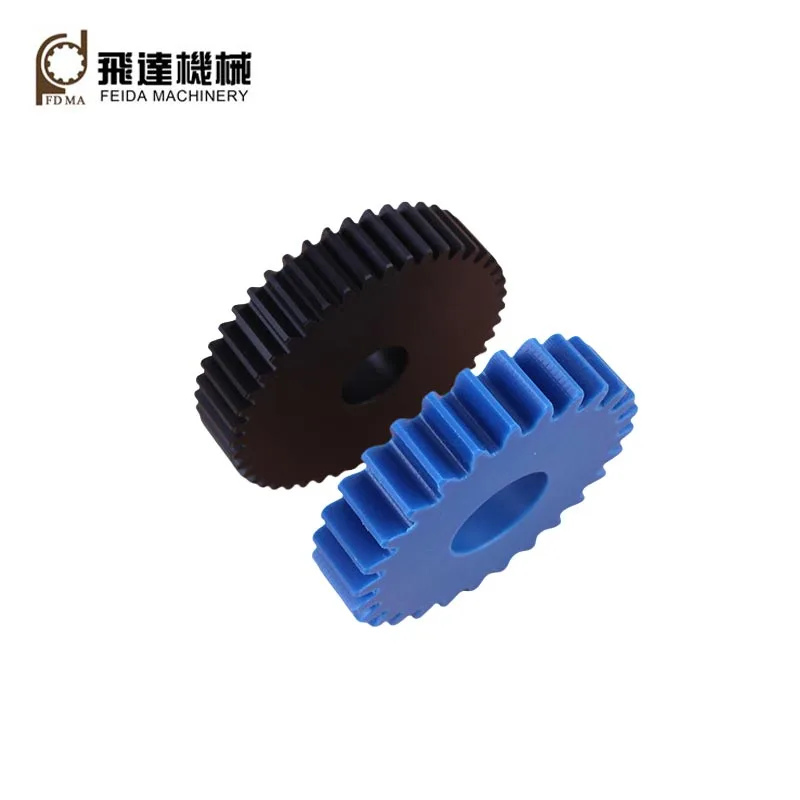
Hot Products
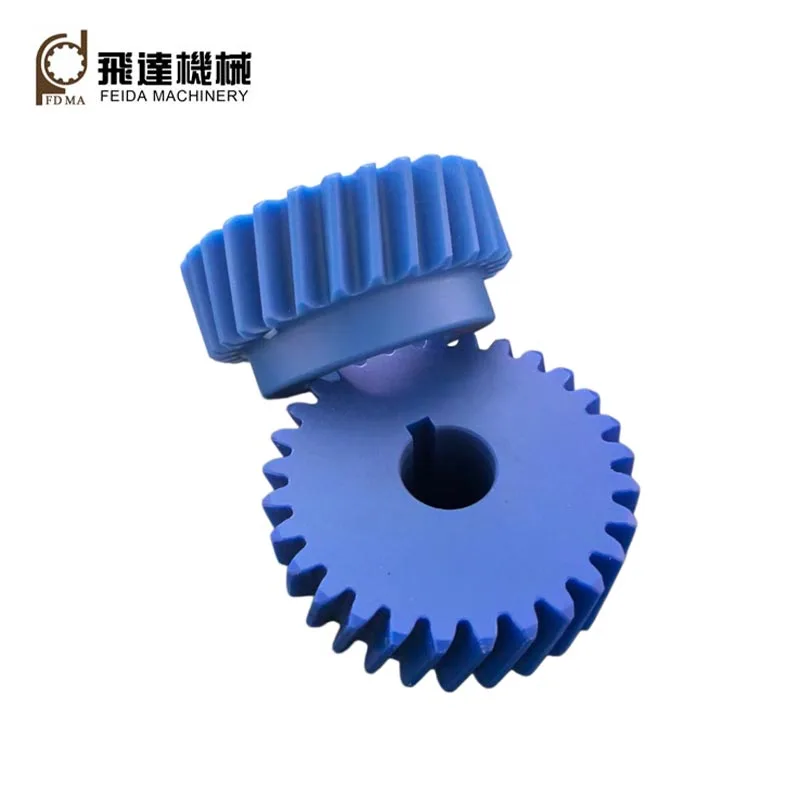
Plastic Helical Gears
High quality raw materials,professional production,and strict quality control allow Feida Machinery factory to supply high-class plastic helical gears to our clients at home and abroad.Whether you have detailed drawings or actual samples, we can work with you to bring your vision to life!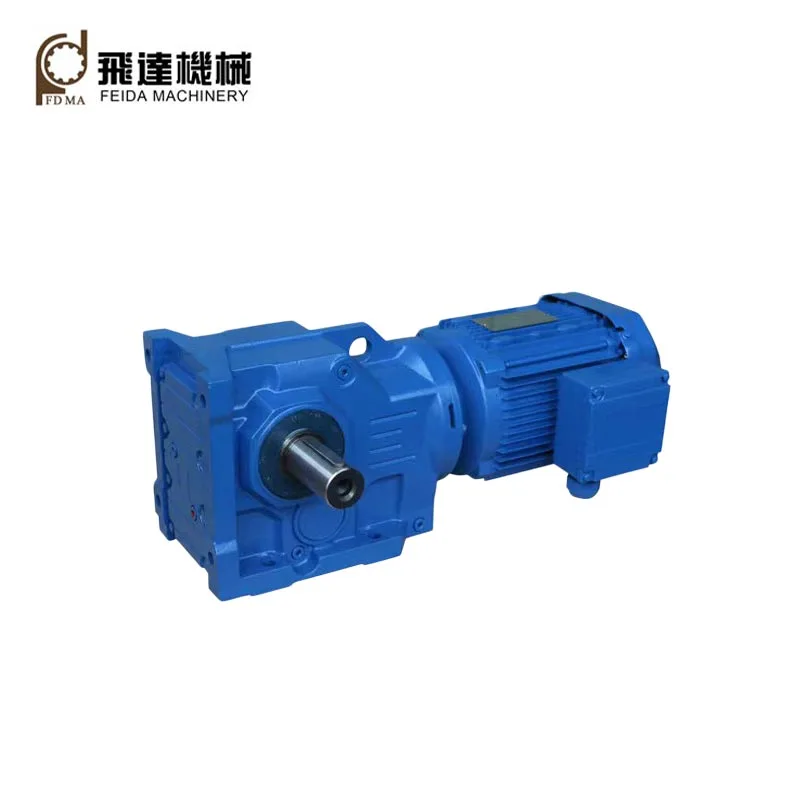
Bevel Gear Reducers
Feida Machinery manufactures and process all kinds of high quality bevel gear reducers since 1988.Welcome new and old customers to continue to cooperate with us to create a better future!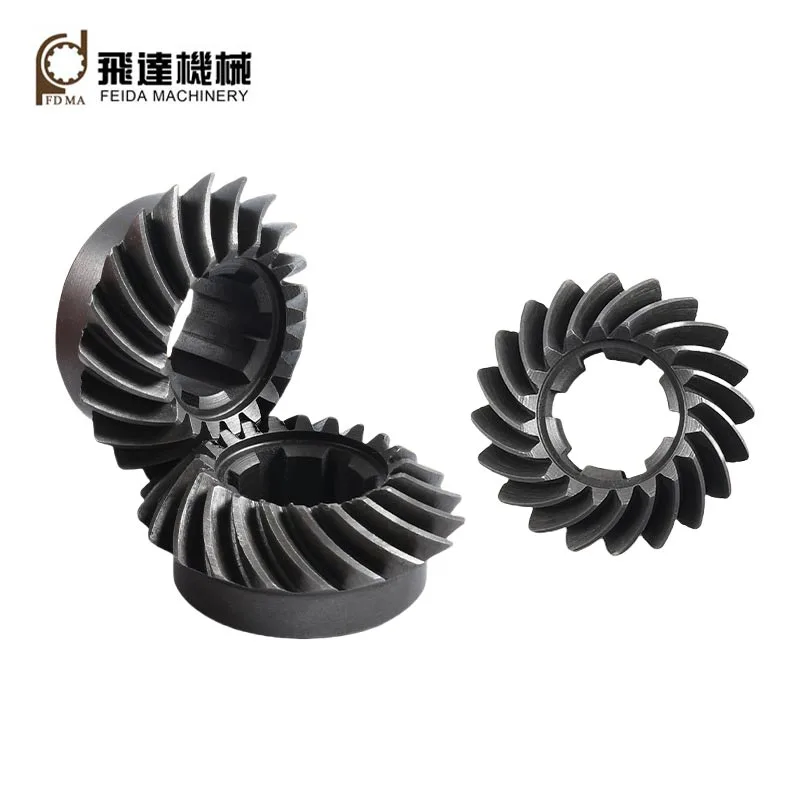
Spiral Bevel Gears
With more than 30 years' experience, advanced equipment and strict management system, Feida Machinery factory can provide spiral bevel gears for you with stable quality and best service.OEM &ODM is ok ,We are looking forwader to cooperating you!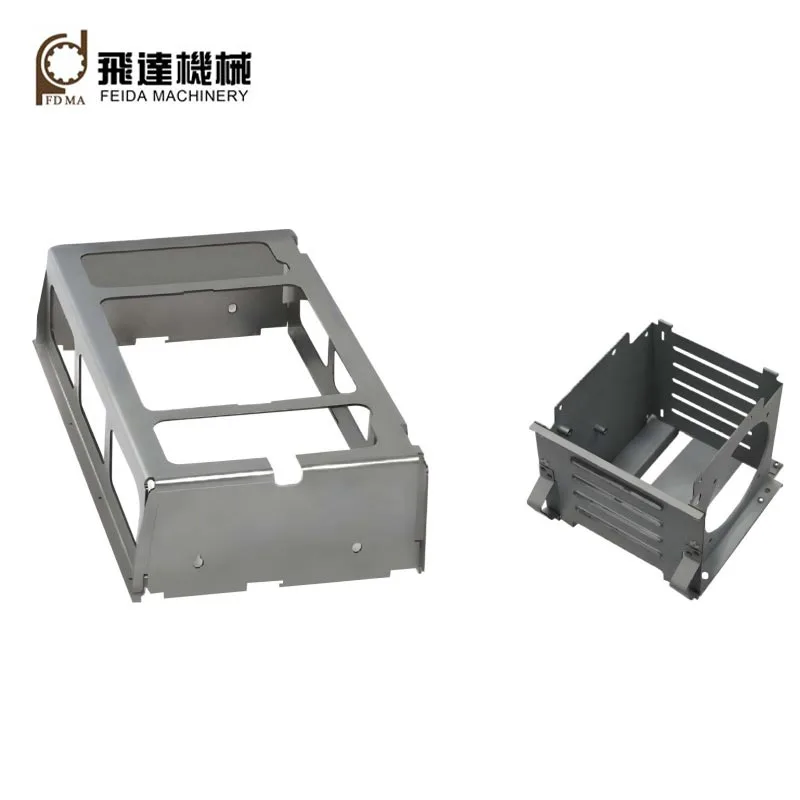
Aluminum Sheet Metal
Jinjiang Feida Machinery Co., Ltd. is a manufacturer and supplier in China who can wholesale Aluminum Sheet Metal parts.Our products have tight tolerlance Min ± 0.1mm and good surface roughness Min Ra 3.2.If you interested in them, please contact with us.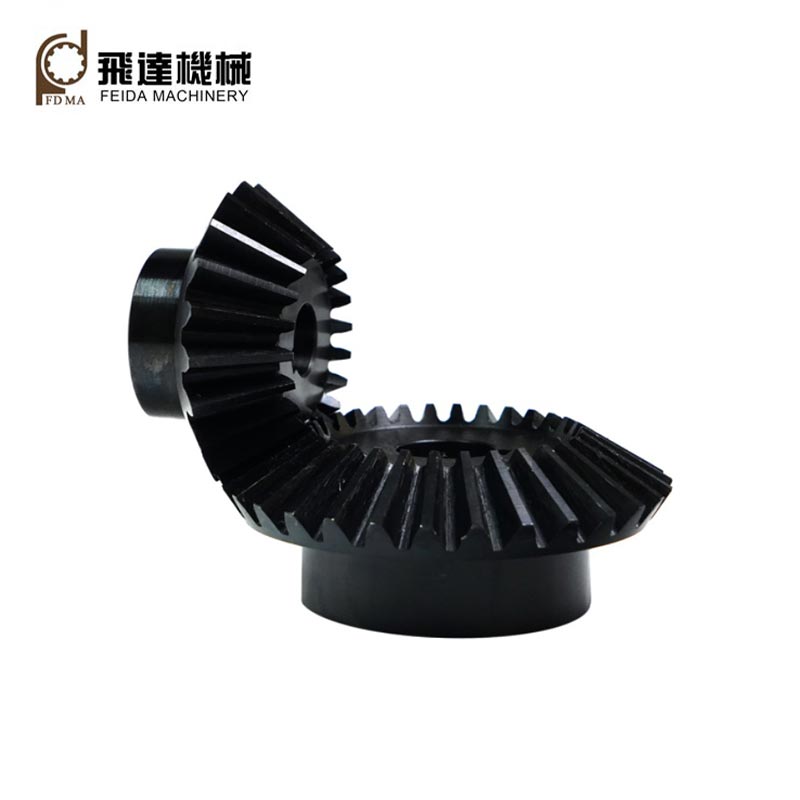
Metal Straight Bevel Gears
With more than 30 years production experience,Feida Machinery produces high quality metal straight bevel gears in its own factory.Our clients are from home and abroad,some of whom also include global 500 enterprises.
We look forward to cooperating with you!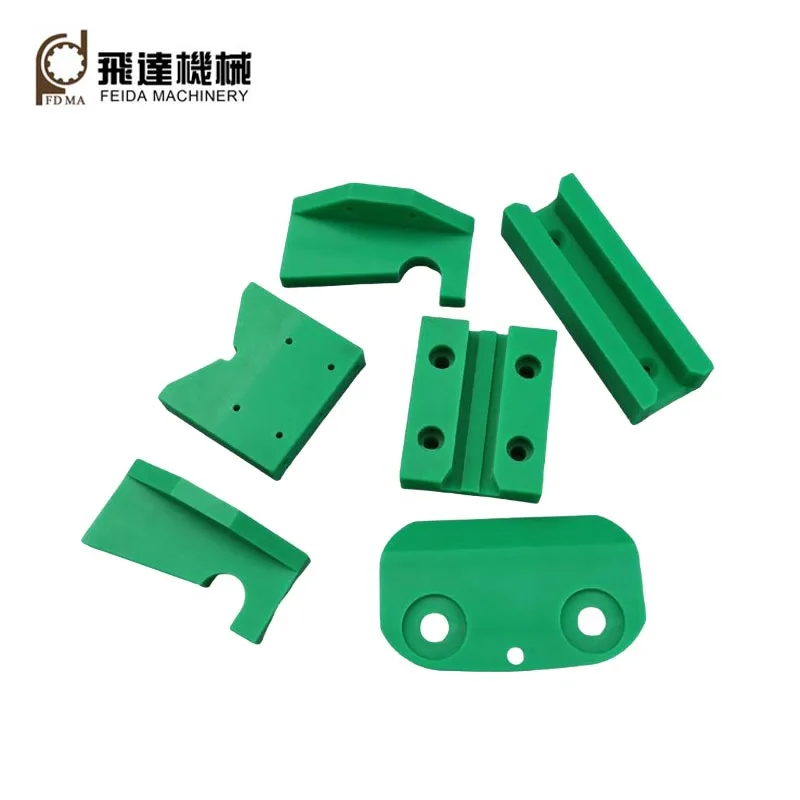
Cnc Plastic Machining
As a china professional manufacturer, exporter,Feida would like to provide you high quality Cnc Plastic Machining parts. OEM and ODM services are acceptable.We welcome to contact us for coopration!
- Related Blog
- Reviews
